






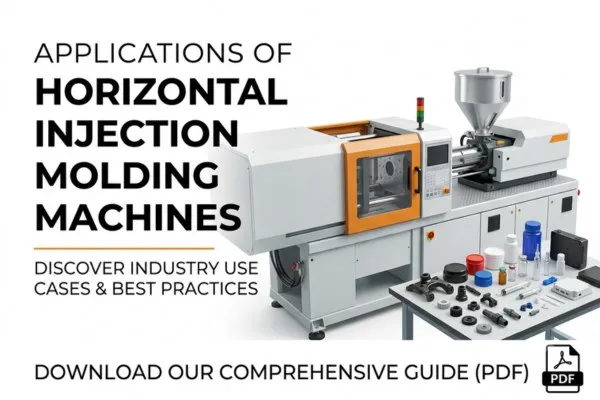

Horizontal injection moulding applications cover nearly every thermoplastic part that can eject free of the mould: buckets and storage boxes, caps and containers, switch plates, toys, automotive clips and trims, and drip irrigation fittings. Before matching your part to a machine, run it through this short checklist.
Quick checklist: is your part a standard horizontal machine job?
| Question | If the answer is no |
|---|---|
| Does the part eject and drop, or get picked, without loading metal inserts every shot? | Compare a vertical machine, which holds loose inserts in place by gravity |
| Does the mould fit between the tie bars of the tonnage you need? | Look at larger or two-platen machines |
| Is the resin a general thermoplastic such as PP, PE, ABS, PC or nylon? | PVC and PET need dedicated screws, and PET preforms a dedicated machine |
| Is the wall a normal thickness for the flow length? | Thin walls need high injection speed, pressure and clamp per cm² |
| Are rejects mainly from size, not shot-to-shot weight drift? | Consider electric injection on a hybrid machine |
Five yes answers mean a standard horizontal machine is the natural fit, and the remaining work is sizing the clamp and shot. One no does not rule it out; it tells you which specification needs extra attention.
Key Takeaways
- The horizontal layout suits automatic running, because parts drop clear or are picked by a robot and moulds change on one axis.
- The application decides the machine through three numbers: projected area, tonnage factor of the resin and shot volume.
- Toys and micro-irrigation products in India come under BIS standards, so the process must hold the dimensions those standards test.
- Small parts on an oversized machine waste energy; spread work across tonnage bands that fit each family.
Which horizontal injection moulding applications fit a standard machine?
Household goods, packaging, electrical accessories, toys, automotive components, agricultural and irrigation parts and general engineering parts. What they share is a part that ejects free of the mould without hand-placed inserts, in a resin that runs on a general-purpose or material-specific screw.
The table groups the families by what usually decides the machine for them. A housewares unit sizes for projected area and shot weight; a closure maker sizes for cavities and cycle; an electrical moulder sizes for the clamp factor of engineering resins and the precision of small features.
Application families and what decides the machine
| Application family | Typical parts | Resin examples | What decides the machine |
|---|---|---|---|
| Household and housewares | Buckets, tubs, storage boxes, chairs | PP homopolymer, PP impact copolymer | Projected area and shot weight |
| Packaging | Caps, closures, containers, pails | PP, HDPE | Cavities, wall thickness, cycle |
| Electrical accessories | Switch plates, boxes, sockets, holders | PC, PBT, nylon | Resin clamp factor, precision |
| Toys | Blocks, vehicles, figures | ABS, PP | Cavities, cosmetic surface |
| Automotive | Clips, trims, ducts, battery cases | PP compounds, nylon | Shot size, mould size |
| Agriculture and irrigation | Emitters, fittings, valves, filters | PP, PE | Cavities, dimensional repeatability |
How does the application change the machine size?
Through the resin and the part footprint. Clamp force is projected area times a tonnage factor that depends mostly on the material and wall, so a PP crate and a PC lamp cover of similar weight can need very different machines. Shot volume then sets the barrel.
A. Urbina, writing in SPE Plastics Engineering, gives tonnage factors from 2 to 8 US tons/in² depending on material, with polyethylene at the low end, polycarbonate toward the high end and PP at 2 to 3 tons/in². Without resin data, he suggests 400 bar cavity pressure as a guide value. Long flow paths and thin walls push the factor up within that range.
Our flat opinion: do not run toy-sized parts on a crate-sized machine just because it is free. R. Kent, writing in PlasticsToday, notes that large machines making small products are energy-inefficient, and idling machines have been measured drawing 52% to 97.5% of their full moulding energy. A plant with mixed applications can run better on two or three tonnage bands than on one large press.
Which Indian standards shape common horizontal moulding jobs?
Toys and micro-irrigation products are two clear cases. Toys sold in India must meet BIS standards and carry the ISI mark under a Quality Control Order, and drip and sprinkler components have their own Indian Standards. The moulding process has to hold the dimensions and properties those standards test.
The Toys (Quality Control) Order, 2020 took effect on 1 January 2021 and requires toys to meet seven Indian Standards. These include IS 9873 Part 1 on mechanical and physical safety, covering choking hazards, sharp points and edges, and Parts 3 and 9 on toxic elements and phthalates. For a moulder, that means burr-free parting lines, consistent wall at snap joints and controlled masterbatch.
For irrigation, the BIS compendium lists IS 13487:2024 for emitters, with uniformity categories A and B, IS 17425:2020 for quick-coupled PE pipes and fittings from 40 to 200 mm OD, and IS 18286:2023 for manually operated plastic valves from DN 8 to DN 110. Emitters are small, many-cavity parts where every cavity must flow the same.
When is a horizontal machine not the best choice?
When metal inserts must be placed every shot, when the mould is too large for the tie bars of the tonnage you need, when the job is PET preforms, or when shot-to-shot consistency is the main cause of rejects. Each case suits another machine type better.
Insert moulding favours vertical machines, where loose inserts sit in the lower mould half under gravity. Very large moulds favour two-platen machines, which give more opening for a shorter frame. PET preforms need drying, screw and hot runner equipment built around that resin. Precision multi-cavity parts can justify electric injection on a hybrid.
For everything else, the horizontal layout has practical advantages. Parts fall clear onto a conveyor or are picked by a sprue picker or robot, so the cell can run without an operator at the mould. Moulds are lifted in from above and clamped on one axis, which keeps changeovers simple, and the machine can sit in a straight line with others on the shop floor.
What should you send to match your application to a machine?
Send the part drawing, resin grade, cavities, wall thickness, runner type, mould size, part weight, target output and any Indian Standard the product must meet. With these, clamp, shot and mould fit can be checked before any machine is proposed. See the horizontal injection moulding machine page for the range.
Frequently Asked Questions About Horizontal Moulding Applications
Can a horizontal machine mould PVC pipe fittings?
Yes, with a screw and barrel built for rigid PVC. PVC is heat and shear sensitive, so it needs a streamlined melt path with no dead spots, corrosion-resistant screw metallurgy and careful purging. Never let PVC meet acetal in the same barrel at processing temperature, and never shut down with PVC left in the barrel.
Are horizontal machines used for automotive parts?
Yes. Clips, trims, ducts, brackets and battery containers are commonly moulded on horizontal machines, mostly in PP compounds and nylon. Small clips suit low tonnage with many cavities, while large trims and battery boxes need high tonnage and big platens. Automotive buyers can also expect documented process settings and part traceability.
Which applications need the most clamp force for their size?
Thin-wall packaging and parts in stiff, viscous resins such as polycarbonate. Both push the tonnage factor toward the top of the published range, while polyethylene and PP sit lower. Two parts with the same footprint can therefore need very different machines, so always work out clamp force from the resin and wall.
Can drip emitters run in high-cavity moulds on a horizontal machine?
Yes, and they usually need many cavities to be economical, since each emitter is tiny. The challenge is that every cavity must produce the same flow path, because emitter standards grade uniformity. That puts weight on mould balance, steady injection and close temperature control rather than on clamp force.
Does the application decide the screw design?
Often, yes. A general-purpose screw suits PP, PE and ABS. Rigid PVC needs a low-compression, corrosion-resistant design, and heavily filled or glass-filled grades need wear-resistant metallurgy. Colour-critical parts can benefit from a mixing section. Tell the supplier your main resins before the screw is specified.
Related Articles
- What Is a Horizontal Injection Moulding Machine?
- How Does a Horizontal Injection Moulding Machine Work?
- Horizontal vs Vertical Injection Moulding Machines: Key Differences
- Important Specifications to Consider Before Buying a Horizontal Injection Moulding Machine
Sources & References
- SPE Plastics Engineering, A. Urbina: Mastering Clamping Force Calculation (Mar 2024)
- PlasticsToday, R. Kent: Getting to know your real energy use and cost (Jan 2010)
- BIS Blog: Indian Standards on Toys: Ensuring your child's safety (Apr 2023)
- BIS: Compendium of Indian Standards: Micro-Irrigation Systems
Technical Disclaimer
Disclaimer: The information provided in this document is for general informational and educational purposes only. It is based on technical references and industry information available at the time of preparation and may be subject to change. It does not constitute engineering, technical, commercial or professional advice, nor does it constitute a quotation, specification, warranty or contractual commitment by Pratishna Engineers.
Actual injection moulding machine and process requirements vary according to the component design, material, mould, production volume, machine configuration and operating conditions. The information, examples, calculations and recommendations provided should be independently evaluated and verified for the specific application before making any equipment, process or production decision. Information obtained from third-party sources remains subject to the accuracy and limitations of those sources.
Limitation of Liability: Pratishna Engineers makes no representation or warranty, express or implied, regarding the completeness, accuracy or suitability of the information for any particular application. To the extent permitted by applicable law, Pratishna Engineers shall not be liable for any loss, damage, cost or consequence arising from reliance on or use of the information contained in this document. Final machine selection, configuration and application suitability should be confirmed with Pratishna Engineers based on complete and accurate project requirements.

