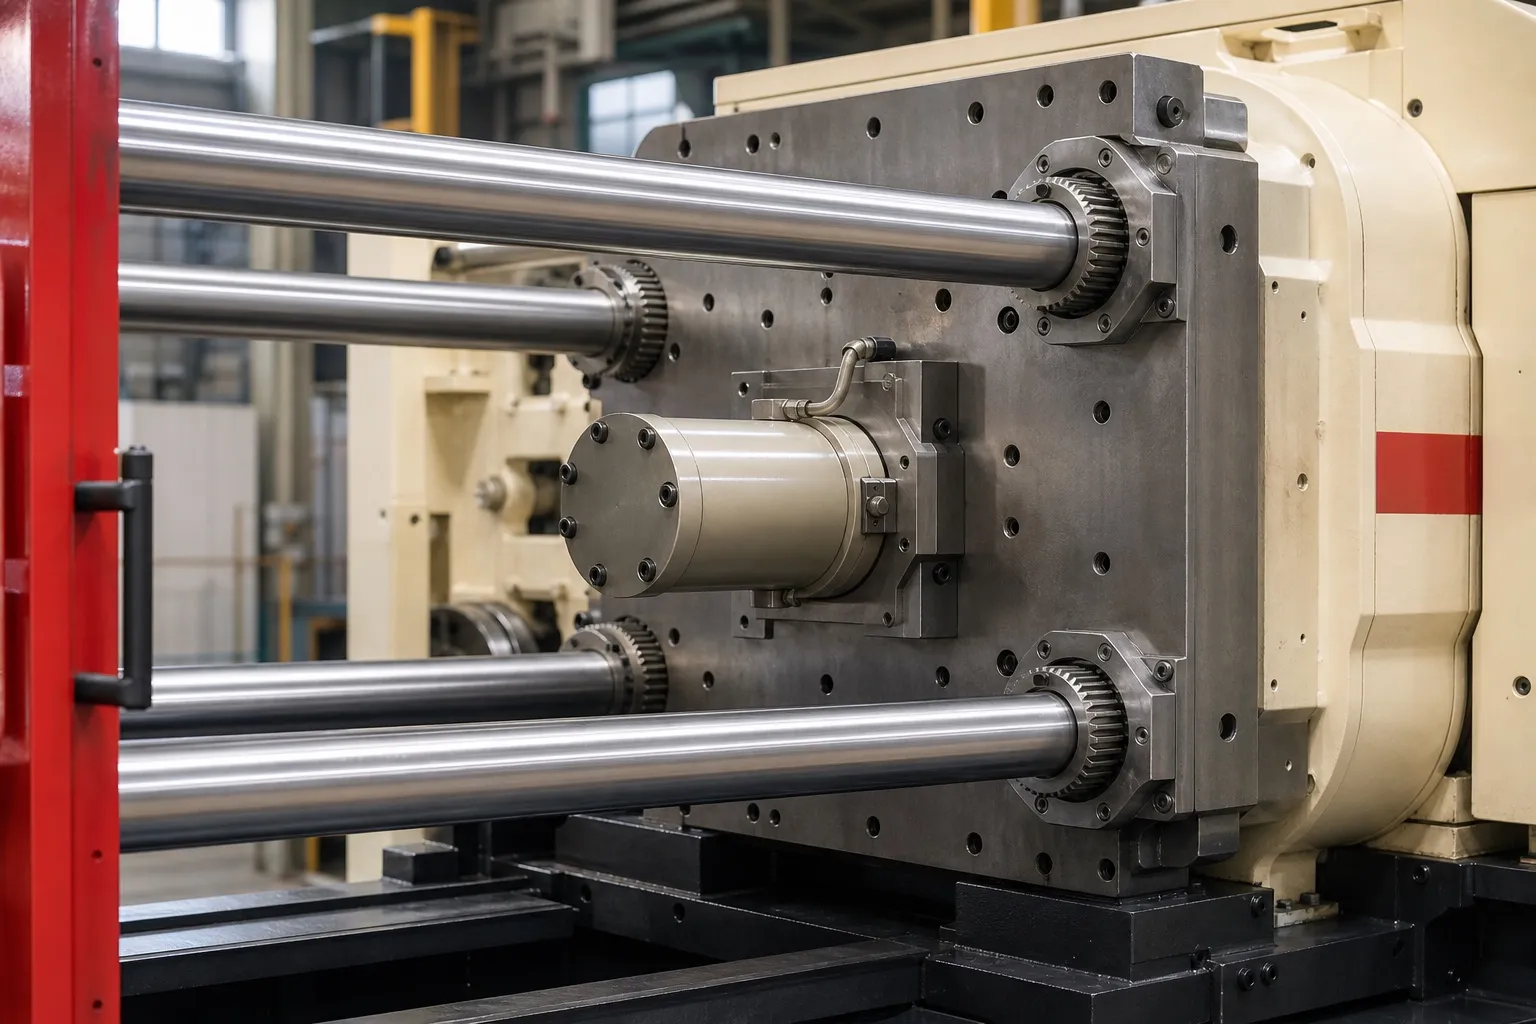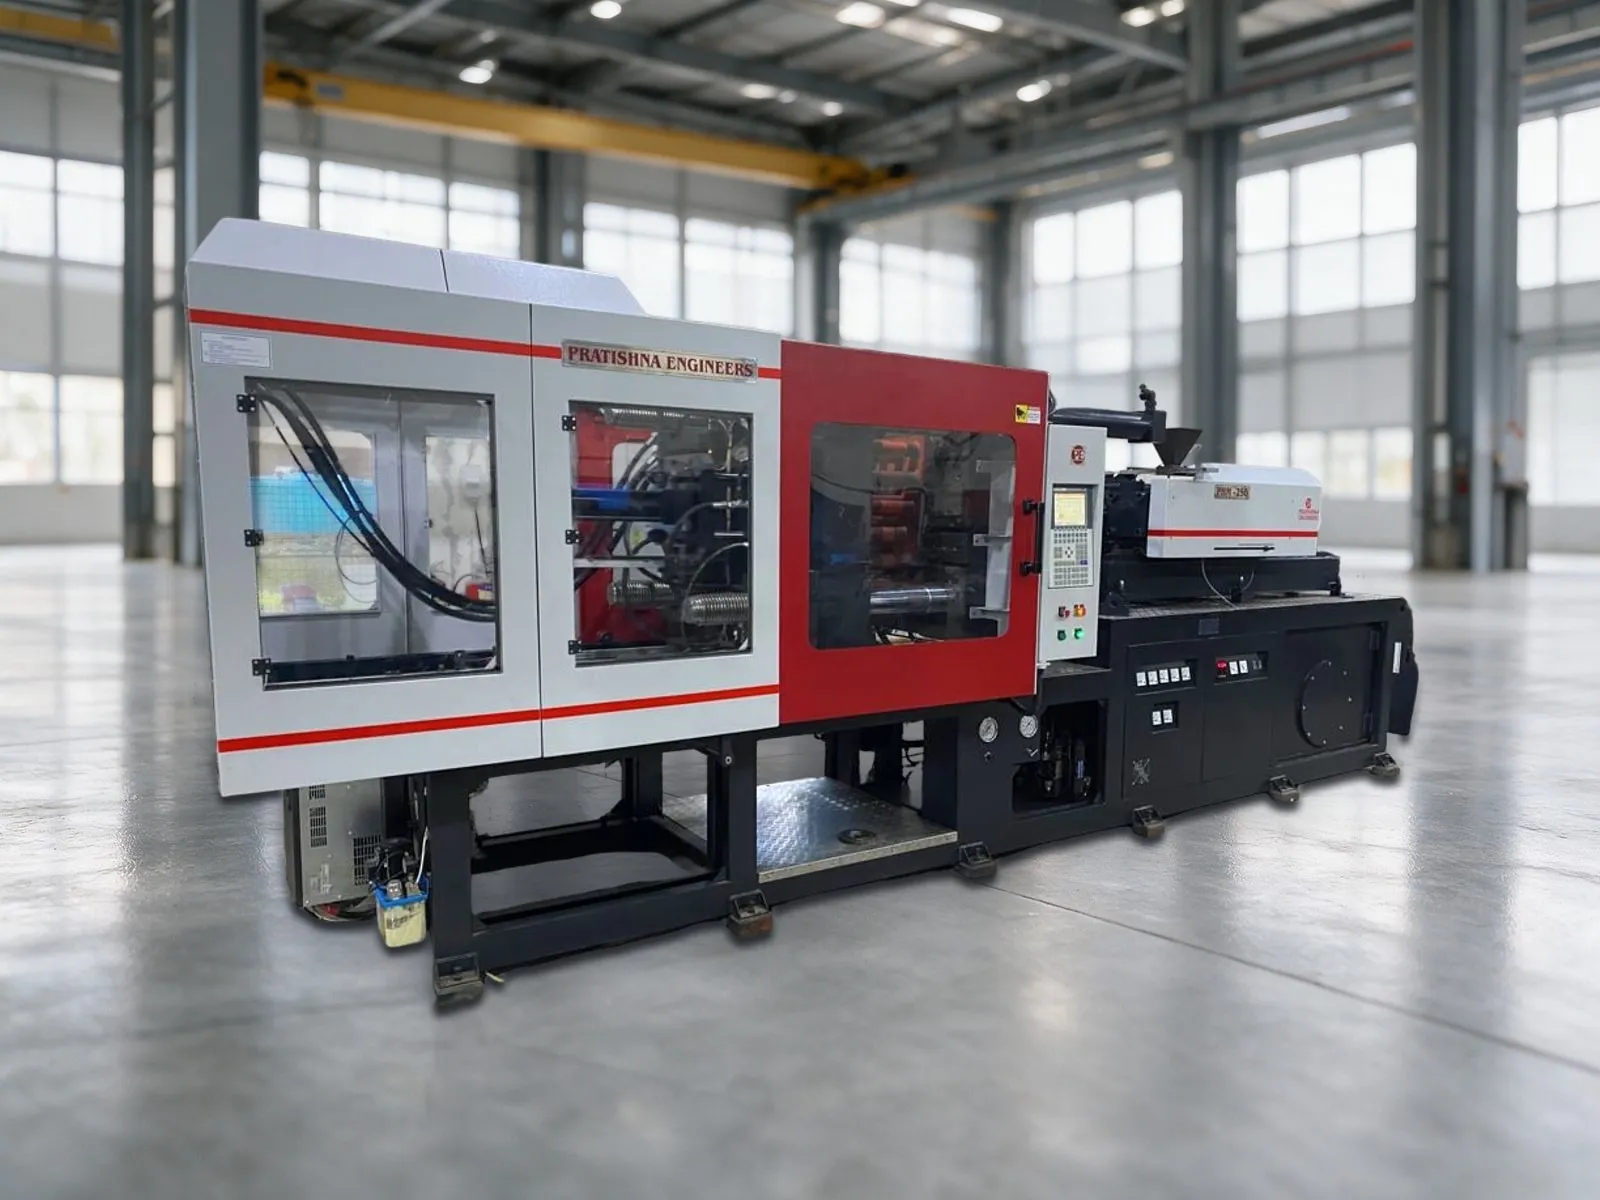

A 350 ton two platen machine suits the largest household and utility parts that still fit one or two per shot: 20 litre paint pails, large dustbins and tubs, medium crates with open bases, stools, small side tables, inverter battery containers and buckets run two at a time. With a 10% reserve (a starting margin, not a rule), it carries about 754 to 1,132 cm² of PP projected area.
That equals one round rim of roughly 310 to 380 mm at PP factors of 3 to 2 US t/in². Crates of 600 × 400 mm, full-size table tops and moulded chairs have larger outlines and need a bigger clamp.
Key Takeaways
- With a 10% reserve, 350 t carries about 754 to 1,132 cm² of PP area, one round rim of roughly 310 to 380 mm.
- A 300 mm paint pail rim fits across the whole PP factor range; a 350 mm dustbin rim fits up to about 2.35 US t/in².
- Two 230 mm buckets per shot need about 257 t to 386 t, so they fit only toward the lower PP factors.
- Paint pails count as rigid packaging and must carry at least 30% recycled content in 2025-26 under India's PWM Rules.
What Can a 350 Ton Two Platen Machine Make?
Pails, large dustbins and tubs, medium crates, stools, small tables and table parts, large battery containers and two-cavity bucket moulds. The table shows the clamp each example needs at PP factors of 2 to 3 US t/in² with a 10% reserve, against the 350 t available.
Clamp needed for typical large parts at 350 t (sizes are assumed examples; PP factor 2 to 3 US t/in²; 10% reserve)
| Part | Projected area | Clamp needed | Fits 350 t? |
|---|---|---|---|
| Paint pail, 300 mm rim | 707 cm² | 219 t to 328 t | Yes, across the PP range |
| Dustbin or tub, 350 mm rim | 962 cm² | 297 t to 447 t | Up to about factor 2.35 |
| Two buckets, 230 mm rim each | 831 cm² | 257 t to 386 t | Up to about factor 2.7 |
| Inverter battery container, 500 × 220 mm | 1,100 cm² | 340 t to 511 t | Only at factor 2 |
| Crate 450 × 300 mm, 40% open base | 810 cm² net | 250 t to 376 t | Up to about factor 2.8 |
| Crate 600 × 400 mm, 50% open base | 1,200 cm² net | 371 t to 557 t | No, a larger clamp is needed |
Crates and tables have their own article in this series, which explains why a full-size table top sits well beyond 350 t. Heavy parts can reach the barrel limit before the clamp limit, which the screw choice article covers.
How Do You Check a Part Against 350 t?
Find the projected area of one part from the parting line, subtract openings that pass right through, multiply by the cavities and add any cold runner. Multiply by a tonnage factor for the resin and wall, convert to tonnes, add a reserve and compare with 350 t.
RJG's John Williams sets out this method in Plastics Technology. He gives a typical range of 2 to 10 US t/in², suggests 3 as a starting point without better data, and names flow length, wall thickness, gate size, gate location and number of gates as the main things that move the factor.
SPE Plastics Engineering's guide by A. Urbina puts PP at 2 to 3 US t/in², with polyethylene at the low end. One US t/in² is 0.1406 t/cm², so factors of 2 and 3 become 0.281 and 0.422 t/cm². At 350 t, 318.2 t usable divided by those factors gives about 1,132 and 754 cm².
Clamp follows area, not depth. A tall dustbin and a shallow tray with the same rim need the same clamp; the dustbin needs more opening, a heavier shot and longer cooling instead.
Count a cold runner in full, because it carries melt at pressure across the parting line; with a hot runner, only the cavities count. On a two-cavity bucket mould, a cold runner across the mould face can add tens of square centimetres, so state the runner type when you ask for a check.
Why Does Opening Matter as Much as Clamp at 350 t?
Because the parts that need 350 t are often tall. A dustbin, a deep crate or a stool must clear its core when the mould opens, and Bruce Catoen's MoldMaking Technology guide sets that opening at a minimum of 2.5 times part height.
A 400 mm dustbin therefore needs about 1,000 mm of opening, on top of a mould that may itself be well over 600 mm tall. The same guide asks that the mould fit within the tie bars, or at least that the parts' projected area does, and that its weight suit both platens.
How a two-platen clamp's opening changes with mould height, and how it compares with a toggle machine, is covered in the two-platen comparison article in this series.
Which Indian Rules Apply to Pails and Large Containers?
Paint pails and other rigid containers count as rigid plastic packaging. Under the PWM (Amendment) Rules notified on 31 March 2026, as reported by Polymerupdate, they must contain at least 30% recycled material in 2025-26, rising to 60% by 2028-29.
Exemptions apply where FSSAI and similar rules restrict recycled content, and shortfalls for 2025-26 can be carried forward up to three years. Dustbins, crates sold empty, stools and tables are not packaging, so the targets do not apply to them, though buyers may still specify recycled blends.
Our view: on a 350 t machine, plan the product mix around one family of parts. A machine that switches weekly between pails with recycled content, food tubs and battery containers spends its spare hours on purging, drying and first-off checks rather than moulding.
What Should You Send for a 350 t Fit Check?
Send the outline, height, wall, part weight, resin grade and cavity count for each part, with through openings marked and the mould maker's estimate of closed mould height. Clamp, opening, tie-bar fit and shot can then be checked together. See the 350 ton two platen injection moulding machine page.
Frequently Asked Questions About Parts for a 350 t Two-Platen Machine
Can a 350 t two-platen machine make a 600 × 400 mm crate?
Usually not. Even with half the base open, the net area of about 1,200 cm² needs roughly 371 t to 557 t at PP factors of 2 to 3 with a 10% reserve. Crates with smaller footprints, such as 450 × 300 mm with an open base, fit.
Can it mould plastic chairs?
A moulded chair's seat and back together usually give an outline far larger than about 1,132 cm², the PP limit at factor 2 with a 10% reserve. That points to a much larger clamp. Stools and chair components such as seats or backs moulded separately may fit, depending on their outline.
Is two cavities better than one at 350 t?
For a part that uses less than half the area limit, two cavities can double output per cycle, as long as the shot, tie-bar gap and mould weight allow it. For a part close to the limit, one cavity with a steady process usually gives more good parts per hour than two run at the edge.
Does polyethylene let me mould a larger part than PP?
Often, because polyethylene sits at the low end of the tonnage factor range. A PE tub can sometimes use the factor 2 limit of about 1,132 cm² where a PP part with a long flow path would need more clamp. Recalculate with the actual grade, wall and flow length.
Which matters more at 350 t, clamp or opening?
Both, but they limit different parts. Wide, shallow parts such as trays and table tops reach the clamp limit first. Tall parts such as dustbins and deep crates often reach the opening limit first, because they need about 2.5 times their height to clear the core.
Related Articles
- Large Crates and Tables on a 350 Ton Two Platen Machine
- Shot Weights Up to 1.5 kg: Screw Choice on a 350 Ton Machine
- When to Choose a 350 Ton Two Platen Over a Toggle Machine
Sources & References
- Plastics Technology, J. Williams (RJG): Clamp Tonnage: More Is Better...Right?
- SPE Plastics Engineering, A. Urbina: Mastering Clamping Force Calculation
- MoldMaking Technology, B. Catoen: Machine Sizing and Specification for Optimal Mold Performance, Part 1
- Polymerupdate, D. K. Jha: India eases plastic recycling regulations (8 April 2026)
Technical Disclaimer
Disclaimer: The information provided in this document is for general informational and educational purposes only. It is based on technical references and industry information available at the time of preparation and may be subject to change. It does not constitute engineering, technical, commercial or professional advice, nor does it constitute a quotation, specification, warranty or contractual commitment by Pratishna Engineers.
Actual injection moulding machine and process requirements vary according to the component design, material, mould, production volume, machine configuration and operating conditions. The information, examples, calculations and recommendations provided should be independently evaluated and verified for the specific application before making any equipment, process or production decision. Information obtained from third-party sources remains subject to the accuracy and limitations of those sources.
Limitation of Liability: Pratishna Engineers makes no representation or warranty, express or implied, regarding the completeness, accuracy or suitability of the information for any particular application. To the extent permitted by applicable law, Pratishna Engineers shall not be liable for any loss, damage, cost or consequence arising from reliance on or use of the information contained in this document. Final machine selection, configuration and application suitability should be confirmed with Pratishna Engineers based on complete and accurate project requirements.