





Blog
Guides and articles from Pratishna Engineers on choosing, sizing and buying injection moulding machines in India.
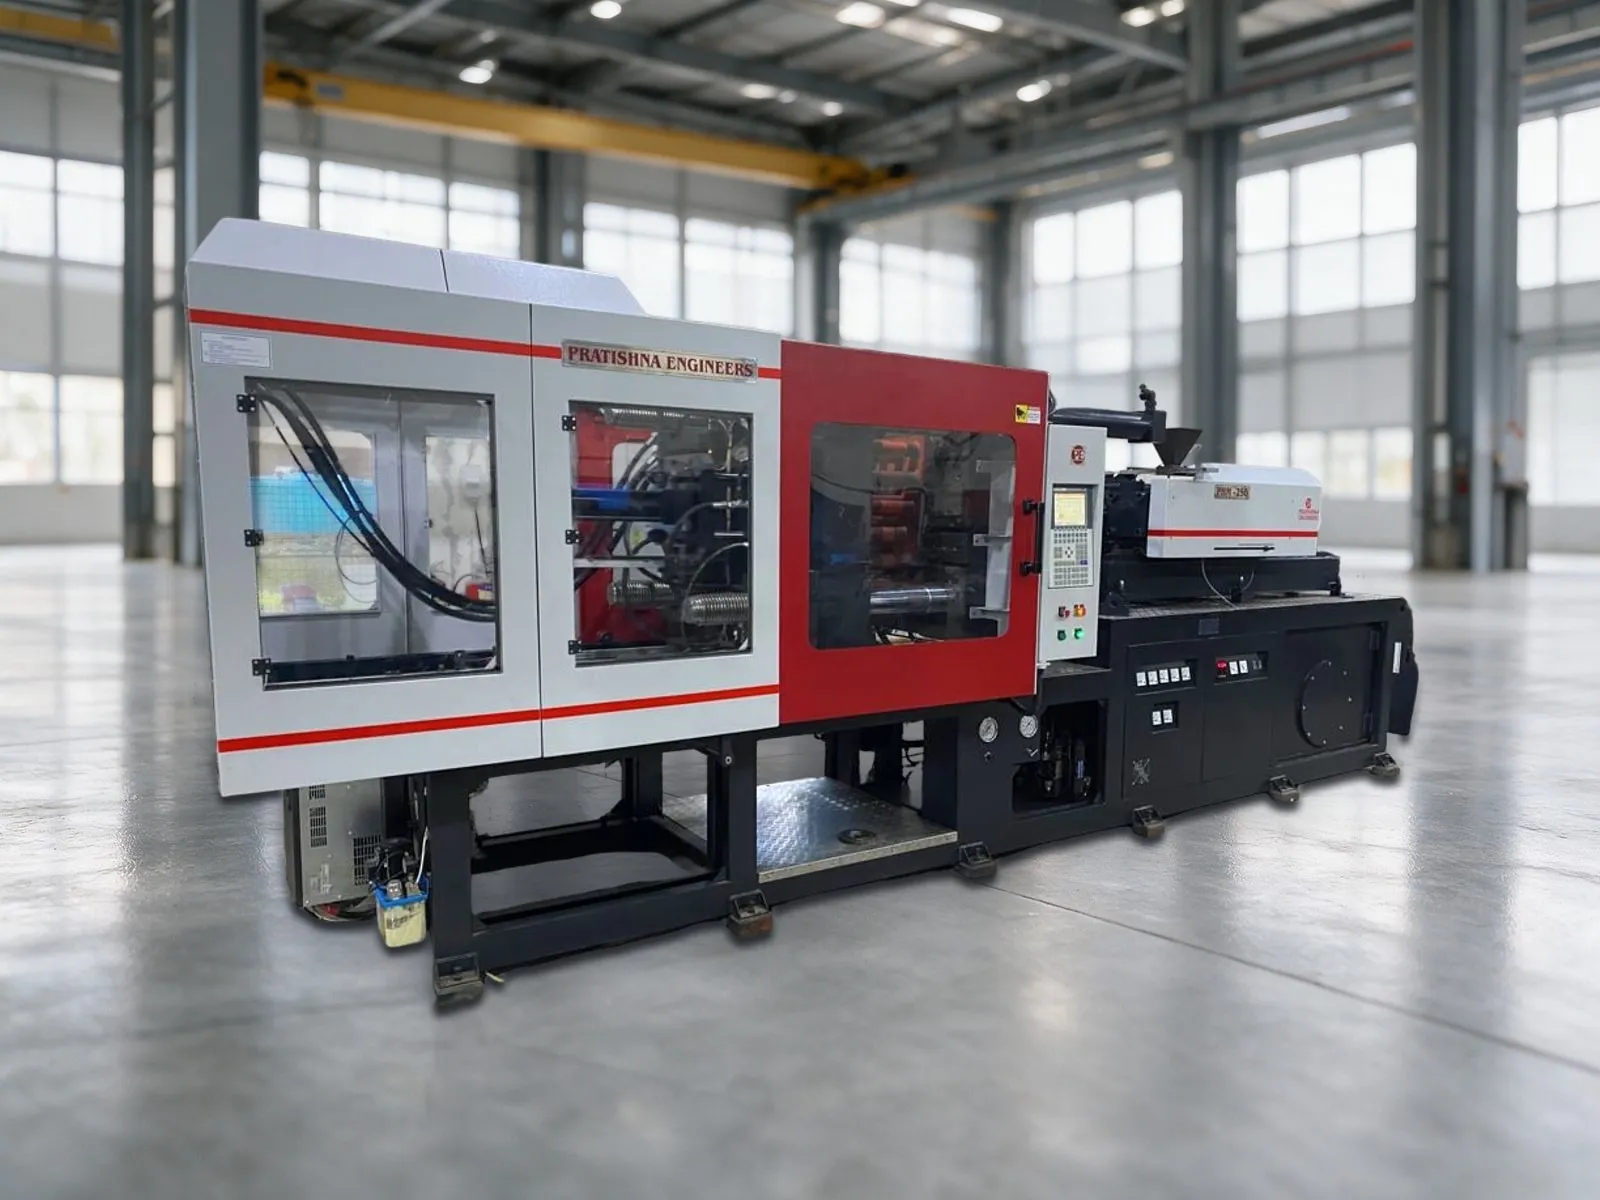
What Can You Make on a 200 Ton Two Platen Machine?
What a 200 ton two platen machine can make: larger buckets, tubs, crates, dustbins and battery containers, plus the clamp sums and limits to check.
Read more
Deep Moulds on a 1000 mm Stroke: Planning Mould Height
Mould height planning for deep parts on a 1,000 mm stroke two-platen machine: usable opening, what makes a mould tall, and the tallest part that fits.
Read more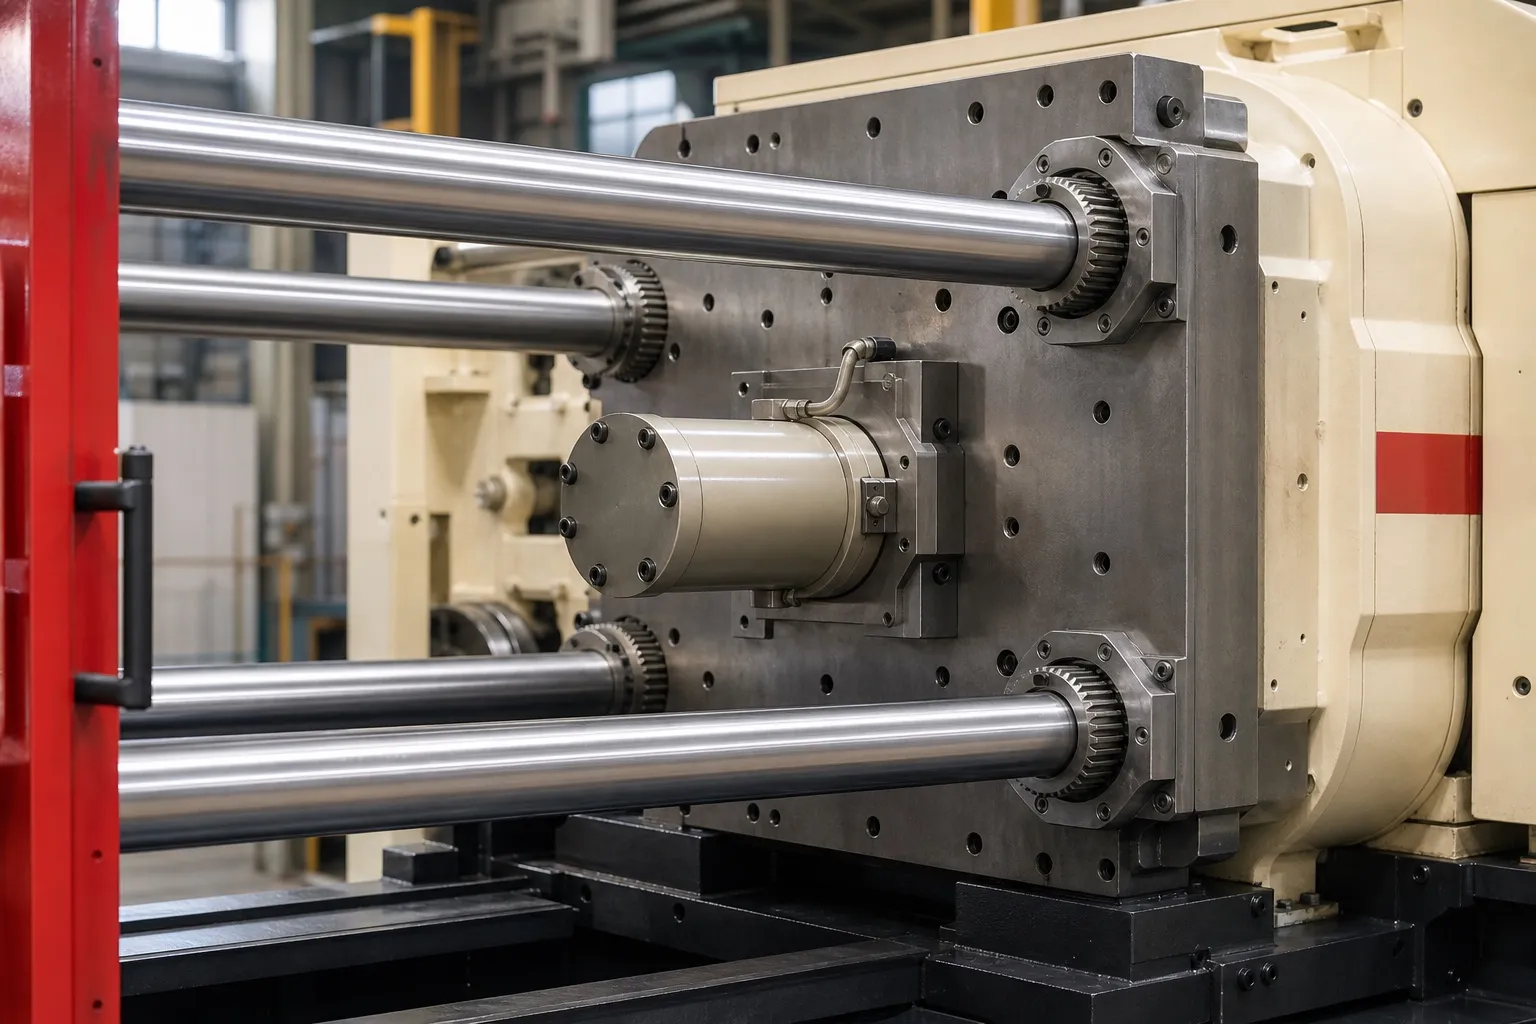
160 Ton Two Platen vs Toggle Machine: Opening Stroke Compared
Two platen vs toggle at 160 t: why a toggle keeps full stroke at every mould height, why a two-platen loses opening as moulds grow, and how to compare.
Read more
Buckets and Storage Boxes on a 160 Ton Two Platen Machine
Sizing a 160 t bucket making machine for buckets and storage boxes: rim size and clamp, barrel and shot, PP grades and recycled content rules in India.
Read moreWhat Can You Make on a 160 Ton Two Platen Machine?
What a 160 ton two platen machine can make: buckets, storage boxes, baskets and deep containers, with the clamp method and the limits that apply.
Read more
Building an Injection Moulding Cell: Robot, Sorting and In-Line Checking
Injection moulding cell automation: what a cell includes, which tasks to automate first, in-line checks and a worked example of good parts per day.
Read more
Shuttle Table vs Rotary Table: When Two Stations Pay Off in Insert Moulding
Shuttle table vs rotary table for insert moulding: how two stations cut cycle time, when they do not pay off, and a worked output example per hour.
Read more
Metal Insert Moulding Around Terminals, Pins and Bushes: What the Machine Needs
Metal insert moulding for terminals, pins and bushes: design rules, hoop stress, common faults and what the machine must do to hold and protect inserts.
Read moreSpecial Purpose vs Standard Injection Moulding Machine: How to Decide
Special purpose vs standard moulding machine: the fit checks to run first, what a special build changes, and when options on a standard machine are enough.
Read more
Post-Mould Cooling and Handling for High-Output Preform Production
Post-mould cooling and handling for preforms: robot cooling time, chilled water, handling marks and neck ovality, and packing at high output.
Read moreSizing a 260 Ton PET Machine for High-Cavity Preform Moulds
High-cavity preform moulds on a 260 t PET machine: cavities by clamp, tie-bar and mould weight checks, shot and injection rate, and running cost.
Read more
Heavy Large-Volume Preforms on a 260 Ton Machine
Heavy large-volume preforms on a 260 t machine: barrel window for a big shot, why the wall sets the cycle, acetaldehyde, and FSSAI rules for water bottles.
Read more
Talk to Our Engineers
Planning a New Injection Moulding Project?
Share your component, material, mould and production target. Our engineering team will help you identify the right machine configuration.
- Machine Sales
- +91 99690 38542
- Service Support
- +91 97689 28259
- Sales Email
- enquiry@pratishnaengineers.com